| Invented scenario | Result | Meaning |
|---|---|---|
| 90 × 70 usable; 20 × 15 part; 1 mm street | 4 × 4 = 16 | Regular orientation only |
| All parts rotated | 5 × 3 = 15 | Not mixed-nesting optimization |
| 16 × 20 × 15 / 6300 | 76.2% | Usable-area denominator |
| 16 positions × 90% yield | 14.4 expected | Not guaranteed delivered quantity |
| 240 / 14.4 | 16.67 currency units | Panel contribution only |
Start with the number of deliverable circuits
Panel utilization can make a ceramic circuit quotation change sharply even when the finished outline changes only slightly. The relevant question is how many usable circuits a manufacturing panel can produce through the agreed process, not simply how much ceramic area appears occupied on a drawing. Separate geometric nesting, manufacturing yield and purchased delivery quantity before comparing quotations. Each has a different denominator and a different source of uncertainty. The ceramic PCB cost guide covers the wider cost structure. This article focuses on the panel assumptions that should accompany a quotation and on how to test whether a proposed outline change produces a real commercial benefit.
Ask which panel the supplier actually processes
A catalog blank, a metallized master card, a fabrication working panel and an assembly array are not necessarily the same object. Ask the supplier to identify the stage to which its panel dimensions refer. Record the material, thickness, process route and available working area for that stage. Rogers discusses multi-unit master cards in its DBC and AMB design guidance, while Anritsu's thin-film designer guide describes substrate blanks with handling borders and saw allowances. These examples demonstrate why one panel rule cannot be transferred automatically between processes. Obtain the current rule for the proposed manufacturing route rather than treating a published example as a universal ceramic standard.
Define the usable rectangle before nesting parts
Start a simple rectangular estimate with the available working width and height after agreed edge exclusions. Confirm whether those exclusions already include the outer cutting allowance, fixture contact, alignment features and process coupons. Counting an allowance twice understates capacity; omitting it overstates capacity. Mark the boundary on a sketch that the supplier can review. For irregular panels or local reserved areas, one rectangle may not represent the available space and a more detailed layout is necessary. The panel yield tool can support an initial comparison, but its result remains conditional on the dimensions and allowances entered by the user.
Use a packing equation with an explicit street convention
For identical rectangular units arranged in a regular grid, define the finished width as w and the clear inter-unit street as g. If the usable panel width is W and no additional outer street is needed within that usable boundary, n units require n times w plus n minus one times g. The largest integer n therefore equals the floor of the quantity W plus g divided by w plus g. Apply the same reasoning to the other direction and multiply the counts. This equation is only a grid estimate. It does not represent arbitrary nesting, process feasibility, tolerances or cutting strategies unless those have already been incorporated in the inputs.
Work through a geometric example
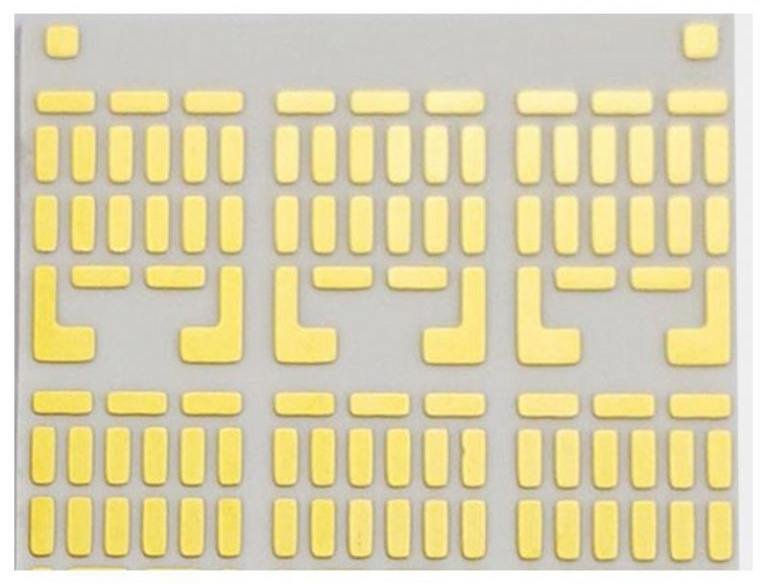
Suppose an invented usable rectangle is 90 by 70 millimeters, a finished unit is 20 by 15 millimeters, and the required inter-unit street is one millimeter in both directions. The first orientation fits four units across and four down, giving sixteen positions. The occupied grid dimensions are 83 by 63 millimeters. Rotating every unit by ninety degrees gives five across and three down, or fifteen positions, with a grid of 79 by 62 millimeters. Neither orientation calculation proves the best possible mixed arrangement. It does show why both regular orientations should be checked before quoting a simple area ratio as the number of circuits per panel.
Label every area percentage by its denominator
In that example, sixteen finished units contain 4,800 square millimeters of ceramic footprint. Dividing by the 6,300 square millimeter usable rectangle gives about 76.2 percent finished-area utilization. If the original gross panel were 100 by 80 millimeters, the same finished units would occupy 60 percent of its area. Both percentages describe the same layout, but they answer different questions. The occupied grid includes streets and is not identical to the sum of finished part areas. State whether a quoted utilization percentage uses gross area, usable area or grid area. Without that label, two apparently inconsistent estimates may simply use different denominators.
Look for step changes rather than continuous savings
The number of units across a panel changes in whole numbers. For the same 90-millimeter usable width and one-millimeter streets, four units can each be at most 21.75 millimeters wide in this simplified model. Increasing that width to 21.8 millimeters makes four units exceed the usable boundary, so only three fit across. If the other direction still fits four, the grid falls from sixteen positions to twelve. A very small outline increase can therefore remove a quarter of the positions. These invented numbers illustrate a threshold, not a recommended dimensional target. A production layout also needs the supplier's tolerance and process allowances around that threshold.
Do not design exactly to an unqualified threshold
A nominal fit at the arithmetic boundary may not be a manufacturable fit. Identify whether the panel size, finished outline and street inputs are nominal, minimum or maximum values. Ask the supplier how it accounts for cutting position, edge quality and other relevant variation. Preserve a clear distinction between a commercial nesting sketch and released manufacturing data. If a small outline reduction could add another row, check the mechanical and electrical consequences before accepting it. The circuit may lose attachment area, edge spacing or a mounting feature that costs more to recover elsewhere. Optimization should preserve the functional design and use confirmed manufacturing assumptions.
Evaluate rotation as a process change when necessary
A rectangle can rotate on a sketch without penalty, but a real circuit may have directional features or processing constraints. Review the orientation of vias, alignment marks, trimming access, test probes, cutting sequence and later assembly handling. Consider whether the panel must preserve a common circuit orientation for automated equipment. Rogers' design discussion notes that substrate bending can depend on multiple geometric and construction factors, so a nesting change should also be reviewed in its physical context. Do not conclude that the orientation with the largest geometric count is automatically the lowest-cost production layout. Record any restriction that prevents the apparently better arrangement from being used.
Reserve space for evidence and process control
The fabrication route may require coupons, registration marks, identification or test structures that are not delivered as customer circuits. Ask which reserved areas are already included in the quoted working rectangle and which consume additional positions. A coupon can be essential to establishing the condition of a lot, so deleting it to improve a utilization percentage can undermine the evidence needed to accept that lot. Specify whether customer-specific test features are part of the order and whether they are consumed during inspection. A useful panel estimate identifies these reservations explicitly instead of treating all non-product area as unnecessary waste that can be removed without consequence.
Separate geometric positions from manufacturing yield
A panel with sixteen geometric positions does not guarantee sixteen accepted circuits. Define the acceptance stage for the yield being discussed: patterned substrate, separated circuit, electrically tested part or assembled product. For a purely illustrative planning calculation, sixteen positions at an assumed ninety percent accepted-unit yield produce an expectation of 14.4 accepted units per panel. No physical panel delivers a fractional circuit, and the expected value does not guarantee a delivery quantity. Defects may also be correlated across a panel or lot. Ask the supplier how it plans starts and reserves to meet the purchased quantity, rather than inferring delivery assurance from an average yield alone.
Keep cost examples tied to accepted units
Assume, only for comparison, a processed panel costs 240 currency units and yields sixteen positions. With perfect acceptance, the panel contribution is fifteen currency units per circuit. At the illustrative ninety percent yield, dividing by the expected 14.4 accepted units gives about 16.67 currency units. This excludes setup, inspection, packaging, freight and other charges and is not a market price. If a layout changes the number of positions, it may also change processing cost or acceptance behavior. Recalculate both sides of the comparison rather than holding every other assumption fixed without discussion. The supplier quotation should state which cost basis applies to the actual order.
Distinguish prototype demand from repeat production
A high utilization layout may create inventory that a prototype project does not need. Ask whether the quotation charges a full panel, a minimum lot or a defined number of accepted units, and what happens to excess parts. Also determine whether future orders can reuse the same tooling and panel arrangement. A layout optimized for hundreds of units may not reduce the cost of an order for only a few engineering samples. Conversely, a small initial run can justify a reusable production layout when the design is stable. Separate the development decision from the forecasted production economics instead of allowing a large assumed future quantity to hide the initial commitment.
Review mixed designs with scheduling and traceability
Combining different circuit designs on a panel may improve area use, but it also connects their manufacturing schedules and material requirements. Check that ceramic grade, thickness, metallization and processing sequence are compatible before discussing shared capacity. Identify each design revision and the method used to distinguish separated parts. Consider what happens when only one design changes or one item requires more units than the others. Shared nesting can create excess inventory or delay an urgent replenishment. Its economic benefit should therefore include handling, identification and order flexibility, not just the extra occupied area. Do not call an unapproved mixed panel a ready manufacturing solution.
Request a quotation comparison that exposes the assumptions
Provide the same finished drawing and delivery requirements to suppliers, then ask them to identify their proposed panel approach. Useful comparison fields include gross and usable dimensions, units per panel, orientation restrictions, reserved features, separation method, quantity basis and responsibility for rejected units. A supplier may reasonably keep detailed production yield information private; it can still explain the delivery and pricing terms it is offering. Record assumptions rather than filling missing fields with invented percentages. The manufacturing overview helps connect panel choices to process differences so that a lower unit price can be evaluated against the same scope of supply.
Approve the functional change before accepting the saving
When a supplier proposes a smaller outline or different array, review the change with the people responsible for the assembled product. Confirm that mounting, thermal contact, electrical spacing, test access and packaging still meet requirements. Request an updated drawing and a revised quotation that isolates the change in quantity or cost. Keep the original option available for comparison until the revised design is accepted. A credible panel utilization improvement is one that survives manufacturing review and preserves the intended product function. The final purchase decision should be based on accepted deliverables and a controlled drawing, with geometric estimates retained as supporting calculations rather than delivery promises.
Engineering example
All dimensions, costs and yield assumptions are hypothetical. Supplier review is required before an estimated layout becomes manufacturing data.
Before you release the design
- Identify gross panel and actual usable boundary.
- State street convention and reserved features.
- Check both regular orientations and dimensional thresholds.
- Separate nesting count from accepted-unit yield.
- Compare quotations on the same delivery basis.
Sources and further technical reading
Manufacturer references support the material and process context. Worked examples and checklists are engineering guidance; they are not test results or supplier guarantees.