| Hypothetical geometry | Result | What it establishes |
|---|---|---|
| 20 × 20 positions | 400 connections | Count only |
| 19 × 0.20 mm pitch | 3.8 mm center span | Excludes outer pad extent |
| 19 × 0.80 mm pitch | 15.2 mm center span | No routing feasibility implied |
| (80−60)/2−15 micrometers | −5 micrometers | Full containment not guaranteed; not proof of an open joint |
Define the translation the interposer must perform
A ceramic interposer sits between two connection systems and provides a defined electrical and mechanical translation. That translation may involve pitch, connection order, height, routing layers or the location of external terminals. Begin with both mating interfaces rather than a ceramic material name. Identify which side receives a die or package and which side connects to the next assembly. A drawing that shows only the upper pad array leaves much of the product undefined. The multilayer ceramic circuit guide provides construction context; this article focuses on turning a fine-pitch connection requirement into a manufacturable interposer specification.
Keep the term interposer tied to its actual structure
The same word can describe very different technologies. A patterned ceramic tile with through connections is not automatically equivalent to a silicon interposer or a complete advanced package. Specify whether the proposed product uses surface thin films, co-fired internal conductors, plated holes, filled vias or a combination approved by the supplier. Kyocera describes both co-fired multilayer wiring and thin-film surface processing in its ceramic technology overview. These are distinct manufacturing approaches, and their capabilities should not be mixed into one hypothetical construction. The interposer quotation should identify the route being offered and the interfaces that the supplier actually delivers.
Freeze a connection map before optimizing geometry
Create a machine-readable mapping between every upper terminal and its required lower terminal or internal net. Include power, return, unused and intentionally unconnected positions rather than leaving them implicit. Specify the viewing direction and orientation marks for both faces. A bottom view can easily be mirrored incorrectly when separate organizations prepare mating drawings. Verify the mapping against the intended assembly netlist and preserve revision control. A geometrically attractive fan-out is not useful if it connects the wrong positions. Treat orientation and connectivity as release gates before investing in detailed material comparisons or a reduced pitch demonstration.
Distinguish array pitch from total connection footprint
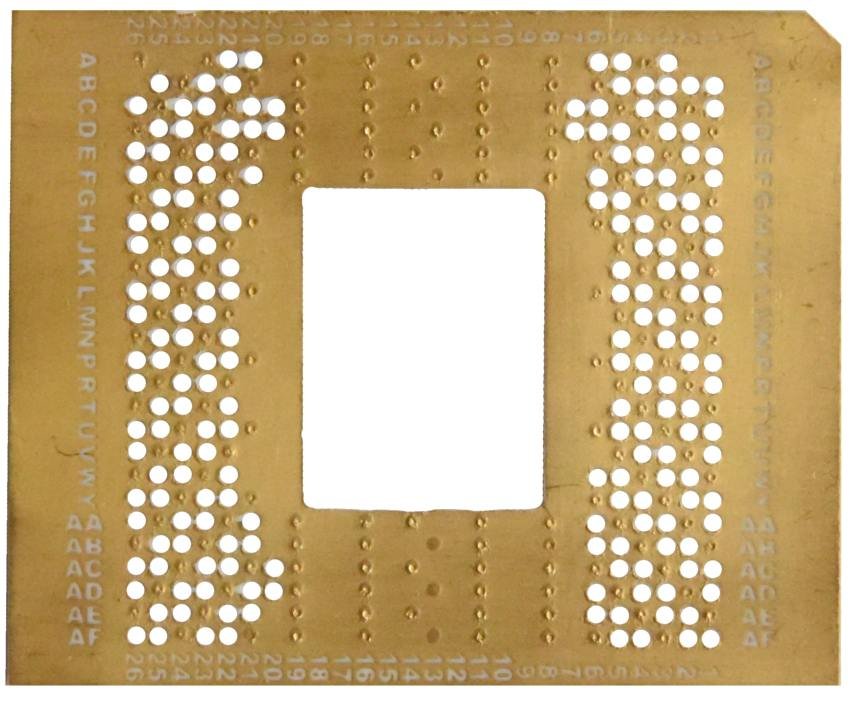
For an illustrative square array with twenty positions in each direction and a center pitch of 0.20 millimeters, the distance between the first and last pad centers is nineteen times the pitch, or 3.8 millimeters. The array contains four hundred positions, but its overall metal footprint also includes pad dimensions beyond those outer centers. At a lower-side center pitch of 0.80 millimeters, the corresponding center span is 15.2 millimeters. These invented dimensions describe a pitch translation only. They do not prove that four hundred routes fit between the interfaces, that every position carries a signal, or that the resulting ceramic outline can be manufactured.
Review finished pads rather than artwork alone
Specify the finished pad shape, dimensions and tolerances at the relevant surface. Clarify how the pad is defined by metal, mask or another controlled feature in the selected construction. Identify the attachment material and mating terminal geometry with the assembler. A nominal drawing pad can differ from the effective attachment area after fabrication and assembly. Do not use a minimum trace capability as a substitute for pad registration or attachment capability. The single-sided ceramic circuit guide describes simpler surface patterns, but a fine-pitch interposer requires explicit control of the relationship between the pattern and both mating components.
Use overlap calculations with a stated acceptance meaning
Suppose an invented one-dimensional containment check uses an eighty-micrometer pad width, a sixty-micrometer mating feature and a possible center offset of fifteen micrometers. Half the difference in widths is ten micrometers, so full containment would have a negative five-micrometer margin at the extreme offset. This does not mean the joint is necessarily open, because partial overlap can remain. It means that full containment is not guaranteed under those assumptions. The assembler must define the required attachment geometry and permissible variation. Extend the assessment to both axes, rotation and actual feature shapes rather than treating this simple subtraction as a complete joint design.
Allocate registration requirements across the interfaces
A fine surface pattern can coexist with a looser relationship to a hole, edge or opposite-side pattern. Applied Thin-Film Products lists these categories separately in its dimensional guidance, reinforcing that they are different manufacturing requirements. Ask for the relevant capability for the complete stack and datum scheme rather than selecting the tightest number from a general capability table. Identify which features the assembly equipment uses for alignment and how those features relate to the functional pads. A ceramic outline tolerance may be irrelevant to optical alignment using fiducials, or critical to a mechanically located assembly. The specification should reflect the actual placement method.
Check routing and vertical connections together
A pad array is only the beginning of routing feasibility. Identify the conductors that must escape between pads and the vertical connections required to reach other layers or the opposite face. Check via land requirements, spacing and layer transitions using the selected process rules. Do not assume every upper pad can connect straight through if the lower pattern has a different pitch or order. Where multiple routing layers are proposed, obtain a feasible stack and representative route review from the fabricator. The double-sided ceramic circuit guide helps distinguish a two-face structure from a multilayer solution with internal routing freedom.
Choose via constructions for their delivered function
A hollow plated hole, a filled connection and a co-fired conductive via can have different geometry, surface condition and assembly implications. State whether an attachment pad lies over a via and what final surface is required there. Identify any concern about attachment material entering an opening or about the local topography beneath a mating terminal. Do not call a via filled without defining the relevant material and finished condition. Confirm inspection access and electrical acceptance with the supplier. A cross-sectional sketch is often more useful than a generic via diameter because it shows how the vertical connection joins the surface pattern and the mating interface.
Preserve return paths and power allocation
The interposer connection map should distinguish signal paths from the associated return and power network. Routing every signal successfully does not establish the electrical behavior of the package. Identify relevant current paths, return transitions and shared impedances for the intended application. If the structure carries high-speed signals, obtain analysis appropriate to its geometry and interfaces rather than inferring performance from ceramic dielectric properties alone. If it carries substantial current, assess the complete conductor and connection path at the relevant temperature. The pad count and pitch describe density; they do not provide a bandwidth or current rating for the finished interposer.
Specify height and coplanarity at the assembly boundary
The spacing between mating assemblies depends on more than the ceramic thickness. Include metallization, attachment layers, terminal height and any other elements in the actual stack. Define the surfaces used to measure coplanarity and the condition in which the requirement applies. A flat bare tile can acquire a different assembled shape after processing or attachment. Review whether the mating component can accommodate the resulting variation without compromising its joints. Do not assign a generic flatness limit merely because it appears on a substrate datasheet. The requirement should come from the attachment process and the functional geometry of the complete assembly.
Consider expansion mismatch over the relevant distance
A small pitch does not eliminate mechanical mismatch between the ceramic interposer and its mating structures. Identify the materials, attachment temperatures and operating excursions relevant to the assembly. The distance from the chosen reference location to a joint can matter when evaluating relative movement, so preserve the actual array size and geometry in the analysis. Do not extrapolate a successful small coupon directly to a much larger interposer without reviewing those differences. The objective is to understand the strain and deformation experienced by the assembled interfaces. Material expansion data can support that work but cannot, by themselves, predict joint life or establish a reliable pitch limit.
Plan inspection before features become hidden
Fine-pitch connections may become inaccessible after assembly. Determine what must be verified on the bare interposer, after the first attachment and after final assembly. Include connectivity, isolation between nets, pad condition, dimensional registration and the attachment characteristics relevant to the process. Choose inspection methods that can resolve the features being accepted, and record their limits. A top-view image cannot establish the condition of every hidden interface. Conversely, a passing continuity test does not prove adequate attachment geometry. Combine evidence according to the actual failure concerns rather than expecting one inspection method to answer every question.
Use coupons that represent the difficult connections
A useful feasibility coupon includes the smallest relevant features, representative vertical transitions and the attachment stack that will be used. It should also expose the regions expected to be difficult, such as dense routing or outer array locations, where applicable. Large isolated pads can demonstrate metallization behavior without proving the fine-pitch assembly. Record which requirement each coupon addresses and what still needs verification on the complete interposer. Preserve its relationship to the production process and material lot when that matters to the evidence. A successful coupon is most useful when its scope is explicit and reproducible.
Compare supplier offers on the same delivered boundary
A bare patterned ceramic, a bumped interposer and an assembled package have different costs, responsibilities and acceptance evidence. State what is included in the quotation and who supplies mating components, performs attachment and accepts the final electrical assembly. Identify tooling, inspection, traceability and engineering changes separately from unit quantity. A proposal for finer surface lines may not include the necessary via, registration or assembly capability. Ask suppliers to mark exceptions against the actual drawing and connection map. This makes the comparison more useful than ranking offers by a single advertised minimum pitch that may refer to a different feature or process.
Release a complete interface specification
The release package should include the connection map, top and bottom views with unambiguous orientation, cross section, material and metallization definitions, finished pad requirements and the approved manufacturing route. Connect these to assembly instructions and the inspection plan for both accessible and hidden features. Record the evidence supporting routing and attachment feasibility and identify any operating limitations. A ceramic interposer is ready for production when the two interfaces and the path between them are controlled together. Fine pitch is one attribute of that product, not a substitute for verified connectivity, geometry and assembly performance.
Engineering example
All pitches and dimensions are illustrative. No supplier minimum pitch, attachment acceptance limit or package electrical performance is asserted.
Before you release the design
- Freeze both interfaces and the mirrored-view convention.
- Verify every connection against the netlist.
- Separate pad, via and front-to-back registration requirements.
- Demonstrate routing and attachment feasibility together.
- Inspect critical features before assembly hides them.
Sources and further technical reading
Manufacturer references support the material and process context. Worked examples and checklists are engineering guidance; they are not test results or supplier guarantees.